
news
Related content
- Oct 28, 2026Winnex Air Rooftop Explosion-Proof Air Conditioner | ATEX Certified Outdoor Rooftop Unit for Zone 1/2 Hazardous AreasThe Winnex Air rooftop explosion-proof air conditioner is designed and manufactured in strict accordance with ATEX Directive 2014/34/EU and the EN 60079 series, and holds an explosion-proof certificate issued by an authorized explosion-proof electrical product inspection body. Explosion-proof marking: Ex db ib mb IIC T4 Gb. The unit serves explosive hazardous locations in the petroleum, chemical, electric power, military and pharmaceutical industries, suitable for Zone 1 and Zone 2 areas where explosive atmospheres formed by Group ⅡA, ⅡB, ⅡC flammable gases or vapours and temperature classes T1–T4 mixed with air may exist. Engineered specifically for outdoor rooftop duty, the unit requires no dedicated machine room and occupies no indoor floor area, making it a rooftop explosion-proof air conditioning solution for centralized air treatment in hazardous-area plants, process units and supporting workshops.
- Oct 27, 2026Winnex Air BKT-200 Explosion-Proof Packaged Air Conditioner | High-Capacity Thermal Solution for Marine & Offshore ApplicationsIn marine vessels, offshore oil and gas platforms, FPSOs and offshore modules, HVAC equipment must withstand harsh marine conditions — salt spray, high humidity, persistent vibration and vessel motion — while complying with explosion-proof safety requirements for hazardous gas areas. The Winnex Air BKT-200 Explosion-Proof Packaged Air Conditioner is a high-capacity, all-in-one thermal unit engineered specifically for these marine and offshore high-risk scenarios. Its packaged design integrates cooling, heating, humidification, steam heating and explosion-proof electrical control into a single unit. Fully tested and explosion-proof certified before delivery, it significantly reduces on-site installation work — ideal for space-constrained marine vessels and offshore platforms.
- Oct 26, 2026Winnex Air Explosion-Proof Air Conditioning System | 50°C High-Temperature Explosion-Proof SolutionThe Winnex Air explosion-proof air conditioning system is engineered for explosive hazardous areas in the petroleum, chemical, electric power, military, pharmaceutical and marine engineering industries, with thermal design and explosion protection specifically addressing 50°C high-temperature environments. The system is designed and manufactured in accordance with ATEX Directive 2014/34/EU and the EN 60079 series. Explosion-proof marking: Ex db mb IIC T4 Gb, suitable for Zone 1 and Zone 2 explosive hazardous areas. Complete explosion-proof technical documentation is available to support HSE review and site acceptance for overseas projects. For industrial projects requiring stable cooling in continuous high temperature, corrosive atmospheres and hazardous areas, Winnex Air provides integrated support from explosion-proof air conditioner selection and technical specification confirmation to maintenance planning.
- Oct 25, 2026Winnex Air Ducted Explosion-Proof Air Conditioner | Concealed Explosion-Proof Ducted Unit for Concealed Air Supply in Hazardous AreasExplore the Winnex Air ducted explosion-proof air conditioner for Zone 1 and Zone 2 hazardous areas. ATEX-compliant design combines concealed ceiling installation, multi-outlet airflow and low-noise operation. Contact our technical team for selection support.
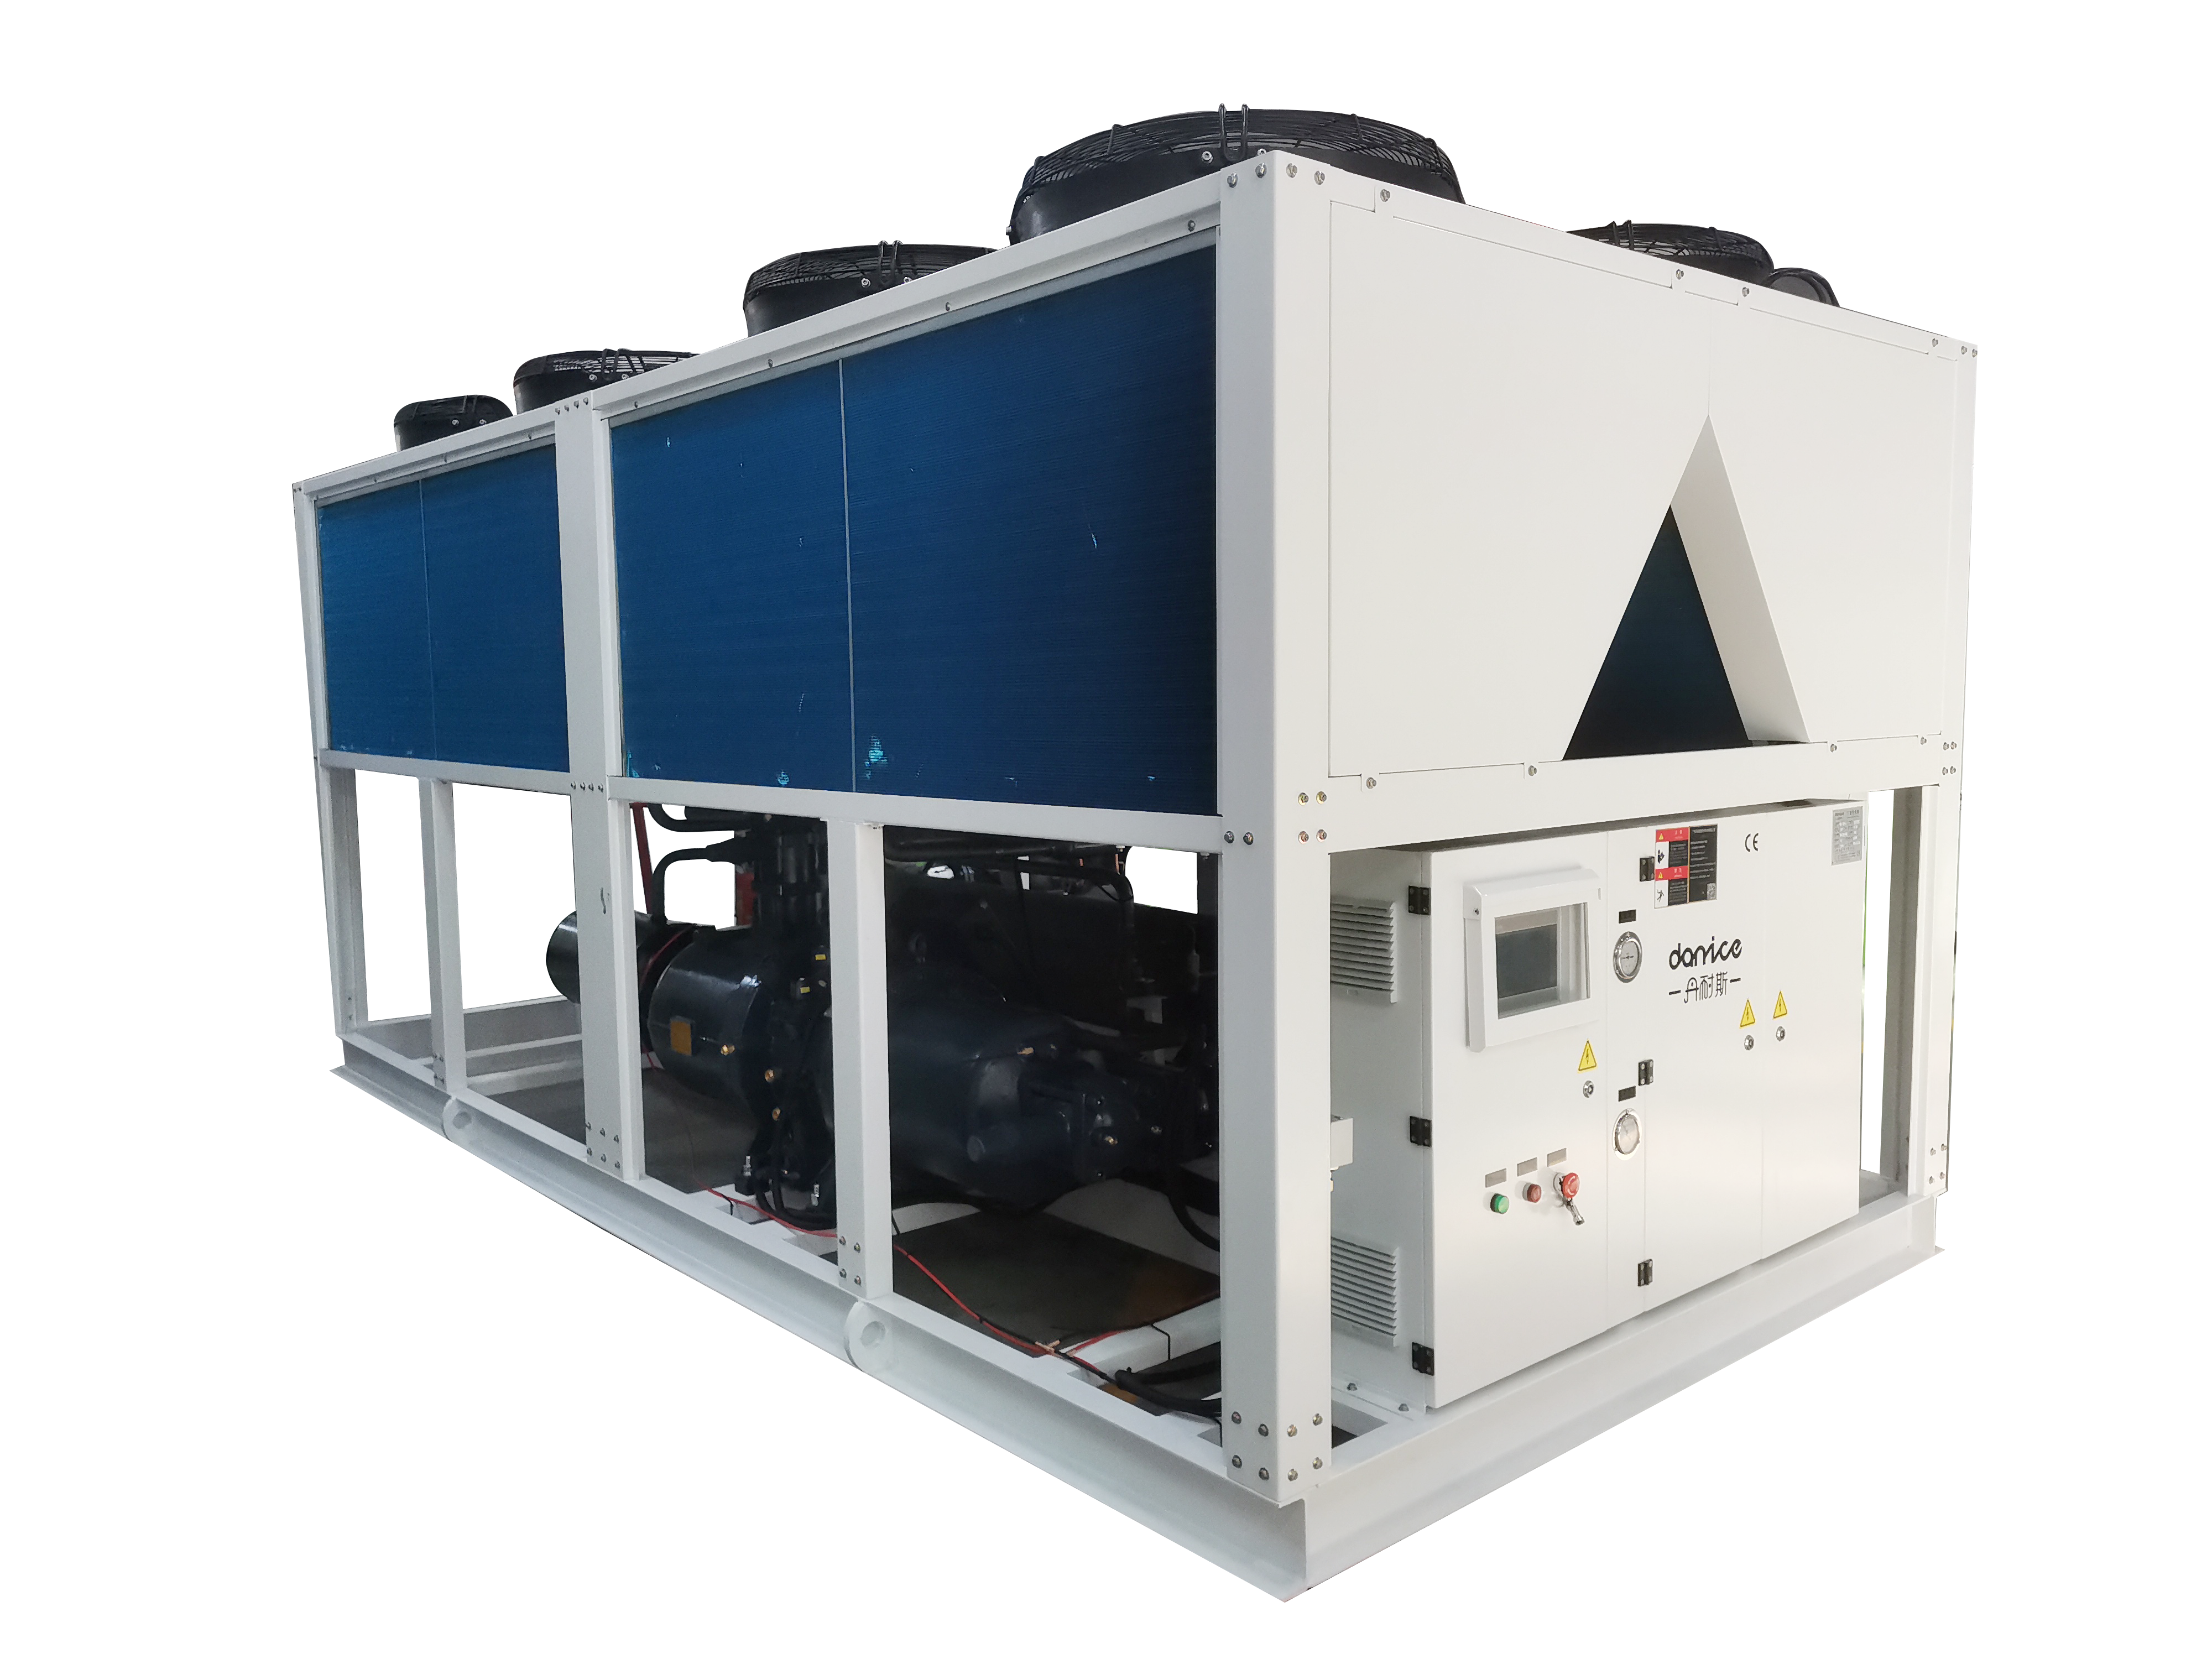
Winnex Air specializes in special industrial refrigeration and high-end HVAC systems, focusing on four core sectors: ATEX explosion-proof industry, marine & offshore engineering, maritime vessel climate control, and data center precision temperature management. Differing from conventional general-purpose HVAC manufacturers, Winnex Air abandons homogeneous mass-produced equipment and adheres to strict standards of extreme condition adaptation, international compliance, long-term reliability and deep customization. We maintain a full-range product portfolio includingindustrial chillers, marine chillers, ATEX-certified explosion-proof cooling units, marine & offshore rooftop HVAC systems, data center precision air conditioners, and industrial constant temperature & humidity units, delivering implementable, fully compliant and low-maintenance one-stop HVAC solutions for global high-risk, harsh and non-standard industrial projects.
1. Full-Coverage Product Portfolio for All Industrial Scenarios
Winnex Air owns a complete industrial refrigeration and HVAC product system that covers diverse industrial demands. Industrial chillers support continuous process cooling for manufacturing plants; marine chillers and maritime HVAC units adapt to anti-vibration, anti-corrosion and 460V/60Hz non-standard power conditions for ocean-going vessels and offshore skid systems; ATEX explosion-proof chillers and HVAC systems fully comply with EU 2014/34/EU directives with original Ex marking, ensuring intrinsic safety in Zone 1 and Zone 2 explosive hazardous areas; data center precision air conditioners deliver ultra-stable temperature and humidity control with minimal fluctuation for critical IT infrastructure; industrial precision HVAC systems serve laboratories, clean workshops and pharmaceutical storage environments. Our integrated product lineup solves all industrial cooling and environmental control challenges with one reliable brand.
2. Original Factory Full Compliance for Global Project Acceptance
To resolve common overseas project pain points such as compliance uncertainty and unqualified modified equipment, all Winnex Air special units are originally designed and fully certified without secondary modification. Explosion-proof products achieve complete ATEX compliance; marine units pass strict salt spray, vibration and high-temperature aging tests; precision climate control equipment meets international data center and clean industry standards. All units are directly applicable for global project bidding, safety audits and final site acceptance, minimizing compliance risks and shortening project construction cycles.
3. Extreme Condition Technology Solves Core Industrial Pain Points
Standard commercial HVAC equipment cannot withstand harsh industrial environments. Winnex Air core technologies are professionally developed for extreme working conditions. Marine and offshore units adopt dual Heresite and electrophoretic anti-corrosion coatings to resist salt spray, high humidity and UV radiation; all series support T3 tropical high-temperature rating to prevent cooling capacity degradation under extreme heat; explosion-proof models adopt full flameproof and increased-safety structural design; marine units feature reinforced anti-vibration and anti-tilt structures for continuous vessel shaking; data center units apply high-precision control algorithms to maintain ultra-stable operational environments for critical equipment.
4. Full-Dimensional Customization for Non-Standard Global Projects
Global overseas industrial projects commonly face limited installation space, non-standard power supply, special static pressure demands, differentiated corrosion grades and exclusive control protocols. Supported by independent R&D and modular manufacturing systems, Winnex Air provides full-scale customization for power voltage, anti-corrosion level, airflow, static pressure, cooling/heating capacity, equipment dimensions, control logic and BMS/SCADA/RS485 communication interfaces, perfectly matching customized requirements of overseas industrial projects, offshore skid facilities and data center renovation projects.
5. Industrial-Grade Durability Reduces Full-Lifecycle O&M Costs
All Winnex Air units are engineered for 24/7 year-round continuous operation, adopting thickened industrial casings, reinforced heat exchangers and premium brand core components with comprehensive electrical protection mechanisms. Whether for full-time data center operation, unmanned offshore platform service or long-term chemical plant production, our equipment maintains ultra-low failure rates and outstanding operational stability, effectively reducing project downtime losses and high overseas maintenance costs to maximize long-term project value.
6. Intelligent Unattended Operation for Modern Smart Industry
All units are equipped with power-fail auto-restart, fault self-lock, intelligent load adaptation and fully automatic precise climate control. Supporting remote monitoring, data logging and automatic fault alarming, our systems can be seamlessly integrated with smart factory platforms, data center central control and offshore SCADA systems. High-level automation minimizes manual intervention and meets modern unattended industrial operation and safety management standards.
7. Full-Lifecycle Global Service System
Winnex Air delivers complete pre-sales, in-sales and after-sales global services, including professional condition analysis, solution design and compliance consultation before sales, full production and quality control tracking during project execution, and remote commissioning, fault diagnosis, technical training and spare parts support after delivery, ensuring stable implementation and long-term reliable operation for global industrial projects.