
Related content
- Oct 28, 2026Winnex Air Rooftop Explosion-Proof Air Conditioner | ATEX Certified Outdoor Rooftop Unit for Zone 1/2 Hazardous AreasThe Winnex Air rooftop explosion-proof air conditioner is designed and manufactured in strict accordance with ATEX Directive 2014/34/EU and the EN 60079 series, and holds an explosion-proof certificate issued by an authorized explosion-proof electrical product inspection body. Explosion-proof marking: Ex db ib mb IIC T4 Gb. The unit serves explosive hazardous locations in the petroleum, chemical, electric power, military and pharmaceutical industries, suitable for Zone 1 and Zone 2 areas where explosive atmospheres formed by Group ⅡA, ⅡB, ⅡC flammable gases or vapours and temperature classes T1–T4 mixed with air may exist. Engineered specifically for outdoor rooftop duty, the unit requires no dedicated machine room and occupies no indoor floor area, making it a rooftop explosion-proof air conditioning solution for centralized air treatment in hazardous-area plants, process units and supporting workshops.
- Oct 27, 2026Winnex Air BKT-200 Explosion-Proof Packaged Air Conditioner | High-Capacity Thermal Solution for Marine & Offshore ApplicationsIn marine vessels, offshore oil and gas platforms, FPSOs and offshore modules, HVAC equipment must withstand harsh marine conditions — salt spray, high humidity, persistent vibration and vessel motion — while complying with explosion-proof safety requirements for hazardous gas areas. The Winnex Air BKT-200 Explosion-Proof Packaged Air Conditioner is a high-capacity, all-in-one thermal unit engineered specifically for these marine and offshore high-risk scenarios. Its packaged design integrates cooling, heating, humidification, steam heating and explosion-proof electrical control into a single unit. Fully tested and explosion-proof certified before delivery, it significantly reduces on-site installation work — ideal for space-constrained marine vessels and offshore platforms.
- Oct 26, 2026Winnex Air Explosion-Proof Air Conditioning System | 50°C High-Temperature Explosion-Proof SolutionThe Winnex Air explosion-proof air conditioning system is engineered for explosive hazardous areas in the petroleum, chemical, electric power, military, pharmaceutical and marine engineering industries, with thermal design and explosion protection specifically addressing 50°C high-temperature environments. The system is designed and manufactured in accordance with ATEX Directive 2014/34/EU and the EN 60079 series. Explosion-proof marking: Ex db mb IIC T4 Gb, suitable for Zone 1 and Zone 2 explosive hazardous areas. Complete explosion-proof technical documentation is available to support HSE review and site acceptance for overseas projects. For industrial projects requiring stable cooling in continuous high temperature, corrosive atmospheres and hazardous areas, Winnex Air provides integrated support from explosion-proof air conditioner selection and technical specification confirmation to maintenance planning.
- Oct 25, 2026Winnex Air Ducted Explosion-Proof Air Conditioner | Concealed Explosion-Proof Ducted Unit for Concealed Air Supply in Hazardous AreasExplore the Winnex Air ducted explosion-proof air conditioner for Zone 1 and Zone 2 hazardous areas. ATEX-compliant design combines concealed ceiling installation, multi-outlet airflow and low-noise operation. Contact our technical team for selection support.
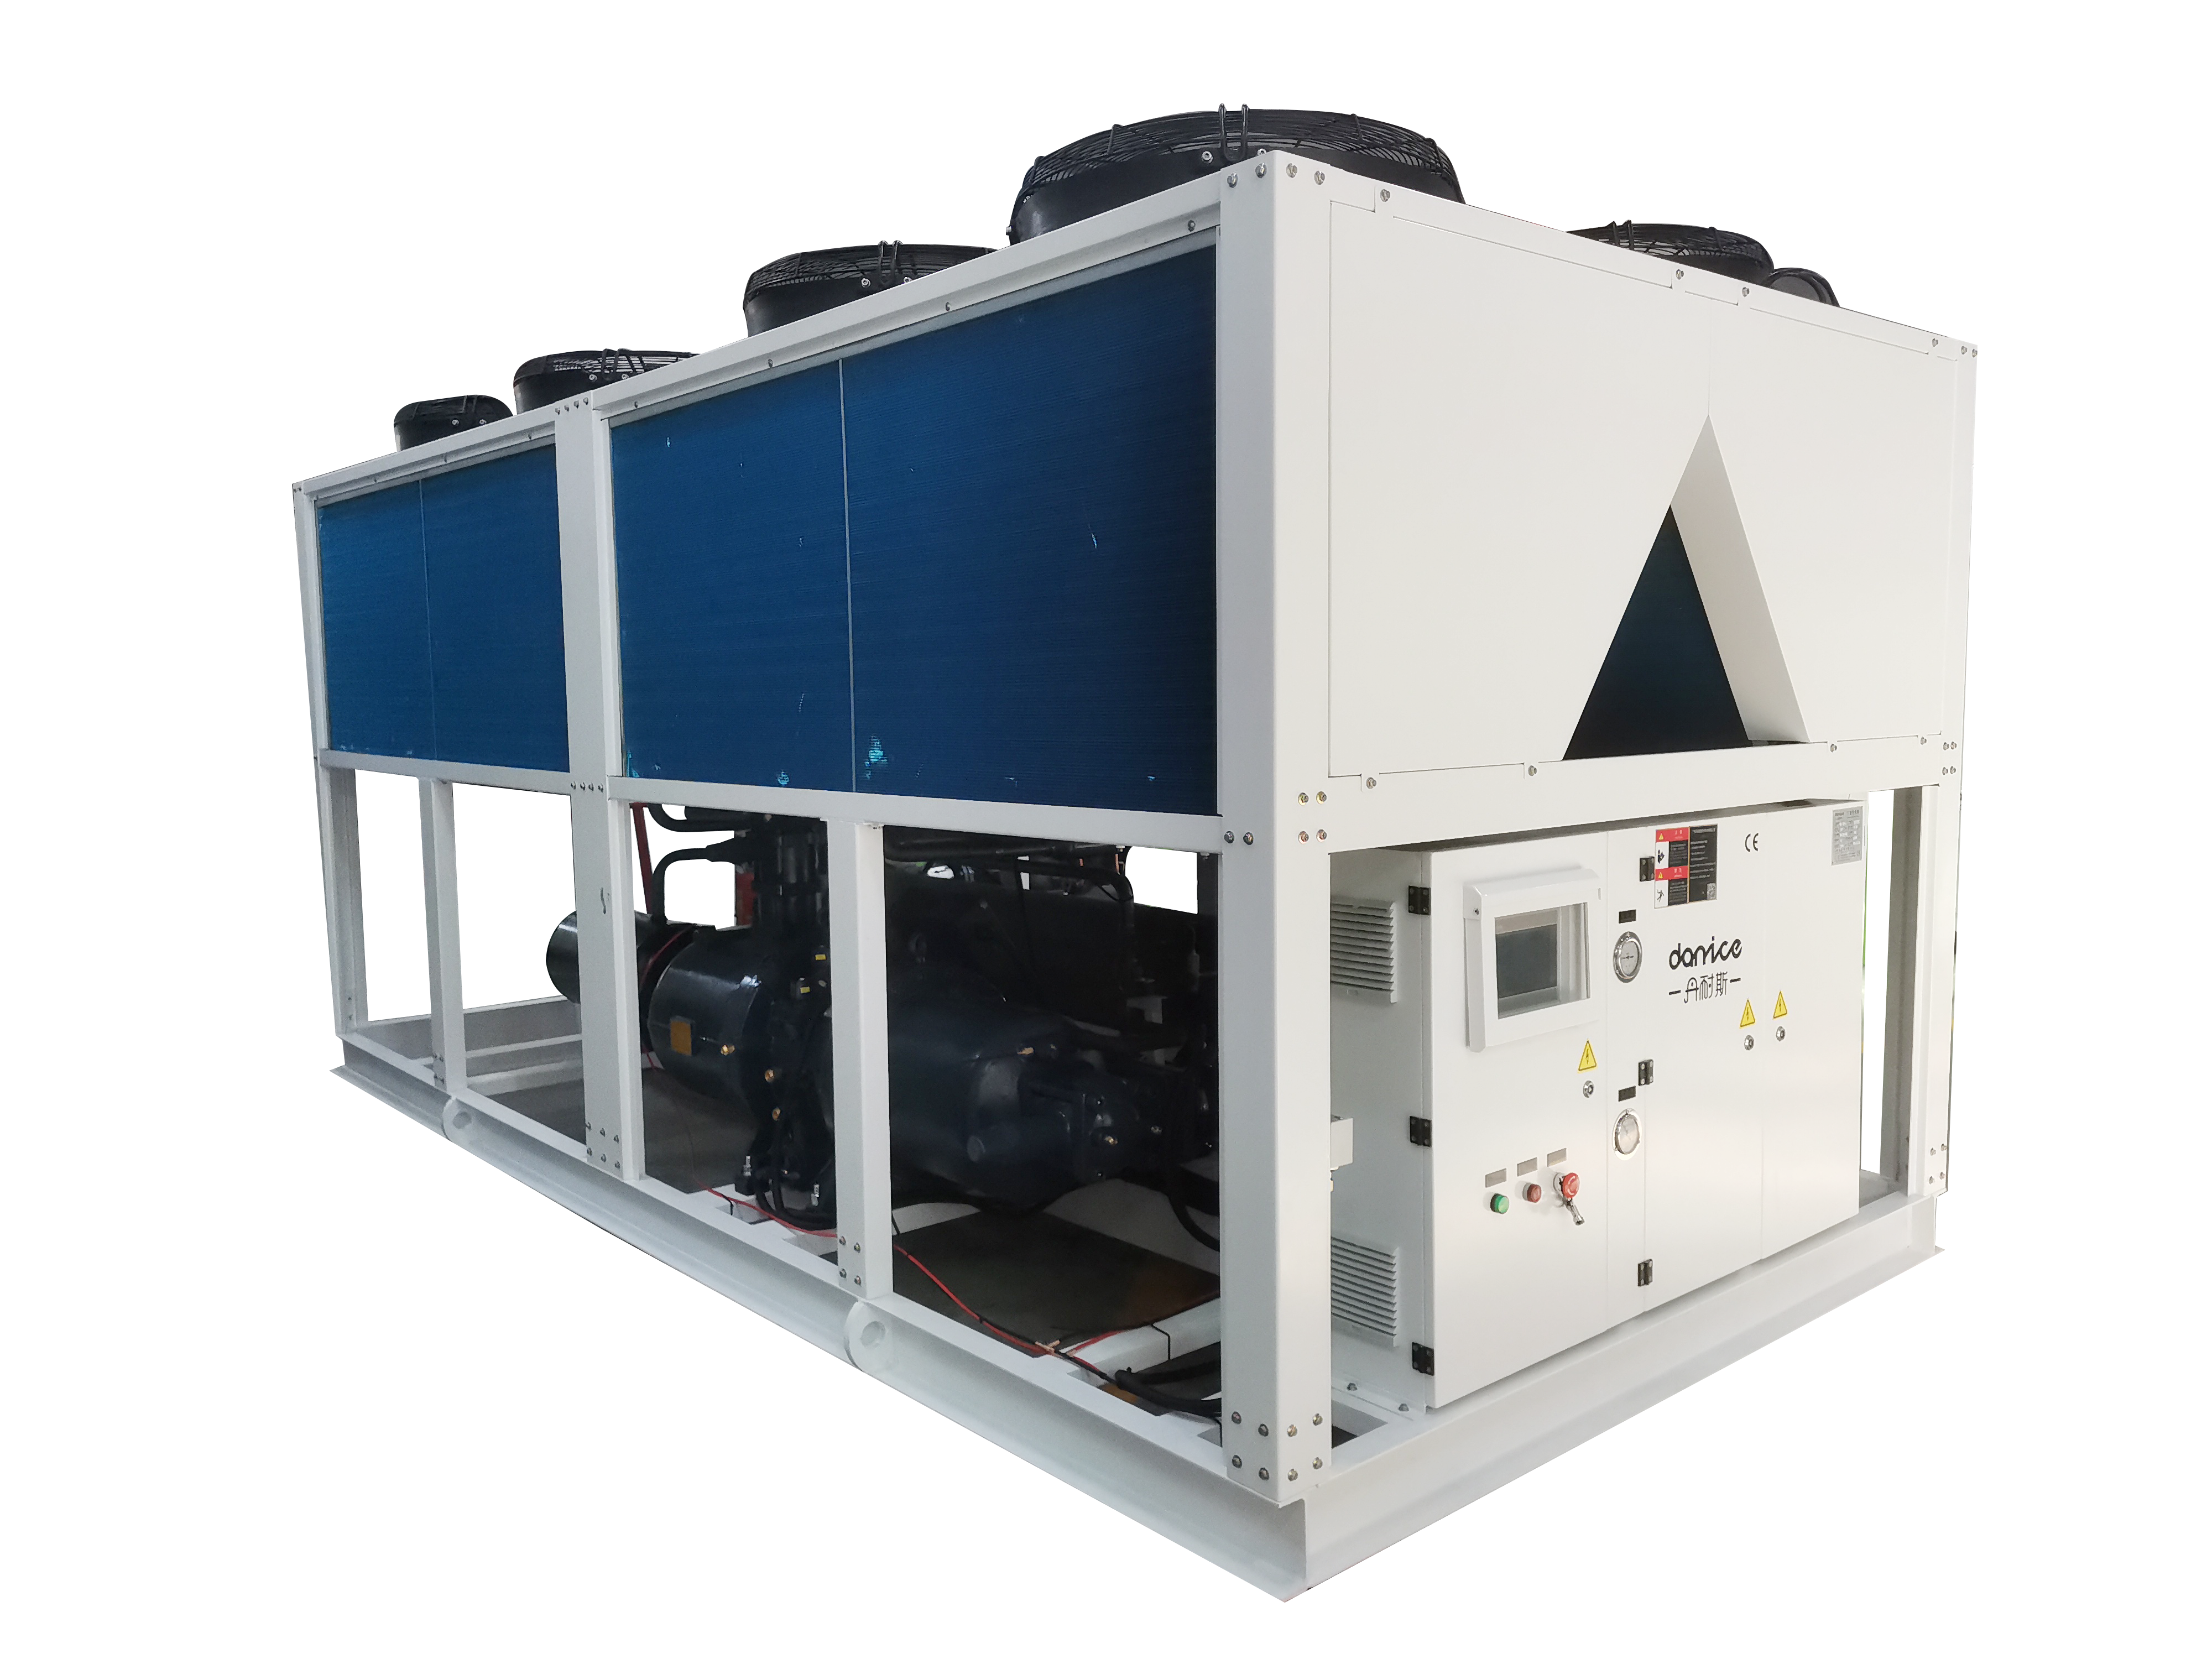
Winnex Air ATEX Certified Explosion-Proof Air-Cooled Chiller fully compliant with ATEX 2014/34/EU directive with official Ex marking, designed for Zone1 & Zone2 explosive hazardous areas for chemical, oil & gas industrial process cooling.
The Winnex Air ATEX Certified Explosion-Proof Air-Cooled Chiller is an industrial-grade hazardous-area cooling solution fully compliant with the European Union’s core explosion-proof standard, ATEX Directive 2014/34/EU. Officially marked with standard Ex explosion-proof marking, the unit is safety-certified for operation in Zone 1 and Zone 2 explosive gas atmospheres, covering petroleum, chemical, oil & gas, biopharmaceutical and flammable industrial production environments.
Different from general industrial chillers, this explosion-proof chiller adopts full-system explosion-proof design on all electrical components, control circuits and mechanical structures, eliminating potential ignition risks caused by electric sparks, overheating and electrical overload. Adopting air-cooled modular structure without cooling towers or water circulation systems, it features flexible deployment, low maintenance and stable 24/7 continuous cooling performance, serving as a standardized, compliant and reliable process cooling solution for global high-risk industrial sites.
Core Compliance Strength|ATEX Certified & 2014/34/EU Compliant
Winnex Air explosion-proof air-cooled chiller isfully ATEX Certified, strictly complying with all essential safety requirements of ATEX Directive 2014/34/EU for equipment used in potentially explosive atmospheres. Equipped with official Ex marking and manufactured in accordance with IEC/EN 60079 international explosion-proof standards, the unit delivers genuine full-machine explosion-proof performance rather than partial modification.
All electrical modules, control units and power components adopt flameproof, increased-safety and explosion-isolated structures, eliminating ignition sources in hazardous areas. It fully meets the strict entry and safety audit requirements of EU offshore projects, cross-border chemical plants and global EPC engineering projects.
Core Product Advantages
1. Full-Machine Explosion-Proof Design for Intrinsic Safety
Compressors, fans, electrical boxes, terminal blocks and sensors adopt professional explosion-proof treatment with high-strength flameproof enclosures. No exposed live parts or high-temperature heat sources effectively prevent flammable gas ingress and eliminate explosion risks. Ideal for chemical processing workshops, reactor cooling, explosion-proof factories and hazardous chemical production areas.
2. Air-Cooled Modular Design, Simple & Flexible Deployment
The integrated air-cooled structure requires no cooling tower, water pump or complex piping system, reducing infrastructure investment and pipeline leakage risks in hazardous zones. Compact footprint and modular parallel operation support flexible capacity expansion, suitable for large-scale centralized process cooling in industrial parks.
3. High-Efficiency Cooling & Wide Working Condition Adaptability
Equipped with high-efficiency variable-frequency scroll compressors and enhanced fin heat exchangers, the unit maintains stable cooling capacity under high-temperature, high-humidity, dusty and slightly corrosive working conditions. Intelligent load adaptive adjustment optimizes power consumption according to real-time process demand, ensuring high energy efficiency for long-term continuous operation.
4. Intelligent Explosion-Proof Control for Unattended Operation
Dedicated explosion-proof controller provides full real-time parameter monitoring with multi-protection mechanisms including overload, overheat, phase loss, high/low pressure and water flow protection. It supports power-fail auto-restart, automatic fault alarm and data logging. Optional RS485 communication enables seamless connection with SCADA and BMS systems for remote monitoring and cluster management, matching modern unmanned factory standards.
5. Enhanced Corrosion Resistance & Long Service Life
The casing and heat exchange system are reinforced with anti-corrosion treatment to resist chemical acid-base gas, dust accumulation and UV aging. Industrial flameproof and temperature-resistant electrical components deliver excellent impact resistance and anti-aging performance, minimizing maintenance frequency and replacement costs for harsh hazardous-area operation.
Application Scenarios
Oil & gas exploitation, petrochemical industry, fine chemical processing, biopharmaceutical manufacturing, new energy lithium battery workshops, hazardous chemical warehouses, offshore EPC projects, and all Zone 1 / Zone 2 explosive gas hazardous areas requiring stable process cooling.